Theory of
Constraints
in Agribusiness
Identifying the single weakest link limiting your weekly farm distribution volume, because more land will not save you if the bottleneck is downstream.
When revenue plateaus, when weekly distribution volumes refuse to grow, when the farm seems to be working harder without producing proportionally more commercial output, the instinctive response is to expand the production base. Plant more hectares. Stock more ponds. Add more birds to the poultry house. The logic feels sound: more production input should yield more revenue output.
Except it does not, when the constraint is not in the field. When the bottleneck sits downstream of production, in a packaging machine that can only process a fraction of harvested output per day, in a cold store too small to hold peak-season volume, in a distribution fleet with insufficient capacity to meet weekly delivery commitments, expanding production upstream of that constraint does not increase revenue. It increases waste. It increases inventory overhang. It increases the gap between what the farm produces and what it actually sells.
This is the central insight of the Theory of Constraints, developed by Israeli physicist and business thinker Eliyahu M. Goldratt and popularized through his 1984 business novel, The Goal. The theory’s foundational proposition is deceptively simple: in any system, one constraint, and only one, limits the system’s overall throughput at any given time. Every other resource in the system operates with surplus capacity relative to that constraint. Improving anything other than the constraint improves nothing at the system level.
Section 01
Core Framework:
Goldratt’s TOC
Goldratt’s Theory of Constraints rests on a single governing metaphor: the chain. A chain’s strength is determined entirely by its weakest link. Strengthening every other link in the chain improves nothing, the chain still breaks at the same point, under the same load. The only productive investment is in the weakest link. Once that link is strengthened, a new weakest link emerges, and the process repeats.
← BOTTLENECK
Starved by constraint
The Five Focusing Steps
The Theory of Constraints does not tell you to improve everything. It tells you that improving anything other than the constraint is, at best, wasted effort and, at worst, a costly distraction from the one action that would actually move your revenue line.
Section 02 — Case Study
The Vegetable Farm That
Planted Its Way Into a Packaging Trap
A commercial vegetable operation in Kaduna State cultivates 34 hectares under drip irrigation, producing tomatoes, bell peppers, and cucumbers for supermarket chains and institutional catering buyers in Abuja and Kaduna city. Over three growing seasons, the owner had progressively expanded cultivated area from 18 to 34 hectares, introduced an improved tomato variety with 40% higher yield per hectare, and invested ₦6.2 million in irrigation infrastructure upgrades.
Weekly dispatch volume had grown from 14 to 19 tonnes per week. But the farm’s buyers had indicated appetite for up to 38 tonnes per week, and the owner could not understand why, despite doubling cultivated area and significantly improving yield per hectare, weekly dispatch had grown by only 36%. A constraint analysis was commissioned.
The Production-to-Dispatch Capacity Audit
| Process Step | Daily Capacity | Weekly Capacity | Utilisation at 19t/wk |
|---|---|---|---|
| Field harvesting (full crew) | 7.2 t/day | 43.2 t | 44% |
| Field-to-packhouse transport | 6.8 t/day | 40.8 t | 47% |
| Washing and sorting station | 5.9 t/day | 35.4 t | 54% |
| Grading table (manual) | 5.4 t/day | 32.4 t | 59% |
| Packaging machine (single unit)CONSTRAINT | 3.2 t/day | 19.2 t | 99% |
| Cold store holding capacity | 12.0 t/day | 72.0 t | 26% |
| Dispatch fleet (3 vehicles) | 8.1 t/day | 48.6 t | 39% |
The constraint was unambiguous. The packaging machine was operating at 99% utilisation across every working day. Every other process step in the chain was running at less than 60% of its capacity. The farm was not limited by land, by yield, by irrigation, by cold storage, or by distribution. It was limited by a single machine running at the edge of its operational envelope, six days a week.
The ₦6.2M Investment History That Made the Constraint Invisible
| Investment Category | Amount | Impact on System Throughput |
|---|---|---|
| Irrigation infrastructure upgrade | ₦3,800,000 | Zero — constraint was not irrigation |
| Improved seed varieties (3 seasons) | ₦1,450,000 | Zero — constraint was not yield |
| Additional harvest labour | ₦620,000 | Zero — harvest was at 44% utilisation |
| Packhouse shelving and storage | ₦330,000 | Zero — storage was at 26% utilisation |
| Packaging machine maintenance | ₦0 | Not budgeted; machine serviced reactively |
| Total invested | ₦6,200,000 | Zero throughput increase beyond machine’s fixed capacity |
Applying the Five Focusing Steps
Step 2 — Exploit: An operational audit revealed the machine sat idle for an average of 47 minutes per day during shift changeovers, lunch breaks, and operator absence. Implementing a staggered break schedule and assigning a designated backup operator eliminated 35 of those 47 idle minutes, increasing effective daily output from 3.2 tonnes to approximately 3.55 tonnes, an 11% throughput gain at zero capital cost.
Step 3 — Subordinate: The grading table upstream was instructed to maintain a maximum buffer of 200 kg of graded product at any time, enough to ensure the machine was never starved of input, but not so much that graded product sat waiting and degrading. The harvest crew’s daily schedule was adjusted to deliver to the packhouse in three staggered batches aligned with the packaging machine’s processing rhythm.
Step 4 — Elevate: With exploitation gains of 11% confirmed and sustainable, a second packaging machine was procured at a capital cost of ₦2.85 million. Combined daily packaging capacity increased from 3.55 tonnes to 7.1 tonnes, a weekly capacity of 42.6 tonnes. Within eight weeks of the second machine entering service, weekly dispatch volume had increased from 19 tonnes to 34 tonnes.
Step 5 — Repeat: With packaging capacity now at 42.6 tonnes per week, the new system constraint shifted to the washing and sorting station at 35.4 tonnes per week capacity, previously comfortable at 54% utilization, now exposed as the binding limit at the new throughput level. The constraint analysis cycle began again.
Section 03
CAPEX Strategy Under
the Theory of Constraints
The standard approach to agricultural CAPEX decisions follows an intuitive but strategically flawed logic: invest where the pain is most visible. Crop losses lead to irrigation investment. Labor costs lead to mechanization investment. Yield disappointments lead to input and seed investment. Each of these decisions may be technically correct in isolation. But if none of them addresses the system constraint, none of them generates additional throughput, and throughput is the only metric that translates directly into revenue.
How Constraints Migrate as Agribusinesses Scale
| Development Stage | Typical Binding Constraints | Management Focus |
|---|---|---|
| Early Stage | Land, irrigation access, working capital, input supply | Secure the production base and financing structure |
| Growth Stage | Harvest labor capacity, post-harvest handling, cold storage | Build logistics and packhouse infrastructure |
| Mature Stage | Processing throughput, packaging, cold chain, distribution, market access | Invest in processing and commercial infrastructure |
Section 04 — Critical Thinking
Physical Asset Constraint
or Staff Training Issue?
This is one of the most consequential diagnostic questions in constraint management, and one that is regularly answered incorrectly, at significant cost. Misclassifying a training constraint as a physical asset constraint leads to capital expenditure on equipment that a better-trained operator would have made unnecessary. Misclassifying a physical asset constraint as a training issue leads to training investment that cannot overcome the hard ceiling of machine capacity.
The distinction rests on a single conceptual clarity: is the limitation determined by the machine’s rated capacity, or by the operator’s ability to extract output from the machine? A machine rated at 4 tonnes per hour operated by an undertrained worker at 2.1 tonnes per hour is not at its physical limit, it is at its operator limit. The same machine in the hands of a fully trained operator may consistently achieve 3.7 tonnes per hour. The gap between 2.1 and 3.7 is a training gap. The gap between 3.7 and 4.0 is a mechanical gap.
The Four-Step Diagnostic Protocol
The Constraint Classification Matrix
| Diagnostic Finding | Constraint Type | Recommended Action |
|---|---|---|
| Expert operator significantly outperforms normal operator | Training | Structured skills transfer, standard operating procedure, operator certification programme |
| Expert and normal operators perform similarly; output below rated capacity | Mechanical | Full service and component inspection before any CAPEX decision |
| Expert operation at rated capacity; rated capacity below throughput target | Physical Asset | CAPEX to elevate, second machine, upgrade, or extended operating hours |
| Output varies significantly day-to-day without clear pattern | Management | Investigate input reliability, shift scheduling, and supervisory coverage at the constraint |
A vegetable packing machine costs ₦2.5M to ₦4M for a semi-automatic unit. A structured operator training program costs ₦150,000 to ₦400,000. If the constraint is a training gap, purchasing a second machine does not solve the underlying problem, it doubles the number of machines being operated below their potential. Run the diagnostic before allocating the CAPEX.
Conclusion
Stop Improving the Chain.
Find the Weakest Link.
The Theory of Constraints is, at its core, an argument for disciplined focus, an argument that more is not better, that broader is not stronger, and that expanding in all directions simultaneously is the surest way to ensure that the one direction that matters most goes unaddressed. In agribusiness, where capital is scarce, seasons are unforgiving, and the cost of misallocated investment is measured in foregone harvests and lost contracts, this argument carries exceptional weight.
Across Nigerian commercial agriculture, in catfish farms where distribution vehicle capacity caps weekly sales well below pond output, in rice mills where milling speed forces WIP accumulation in the receiving warehouse, in poultry operations where cold storage constraints limit the processing of birds already grown and ready, the pattern repeats. Significant investment upstream of an unidentified downstream constraint, producing growth in production capacity that cannot translate into growth in revenue because the bottleneck has never been named.
Goldratt’s contribution was not a complicated algorithm. It was a discipline: before investing, map the system. Measure every link. Find the weakest one. Exploit it fully before spending capital to expand it. Then, and only then, direct investment with precision at the single point where it will unlock the next increment of throughput. The ₦2.85M invested in a second packaging machine generated a 79% increase in weekly dispatch volume within 8 weeks. The preceding ₦6.2M invested upstream generated nothing. Capital directed at the constraint returns revenue. Capital directed away from it does not.
Map your chain.
Find your weakest link.
Everything else is secondary.
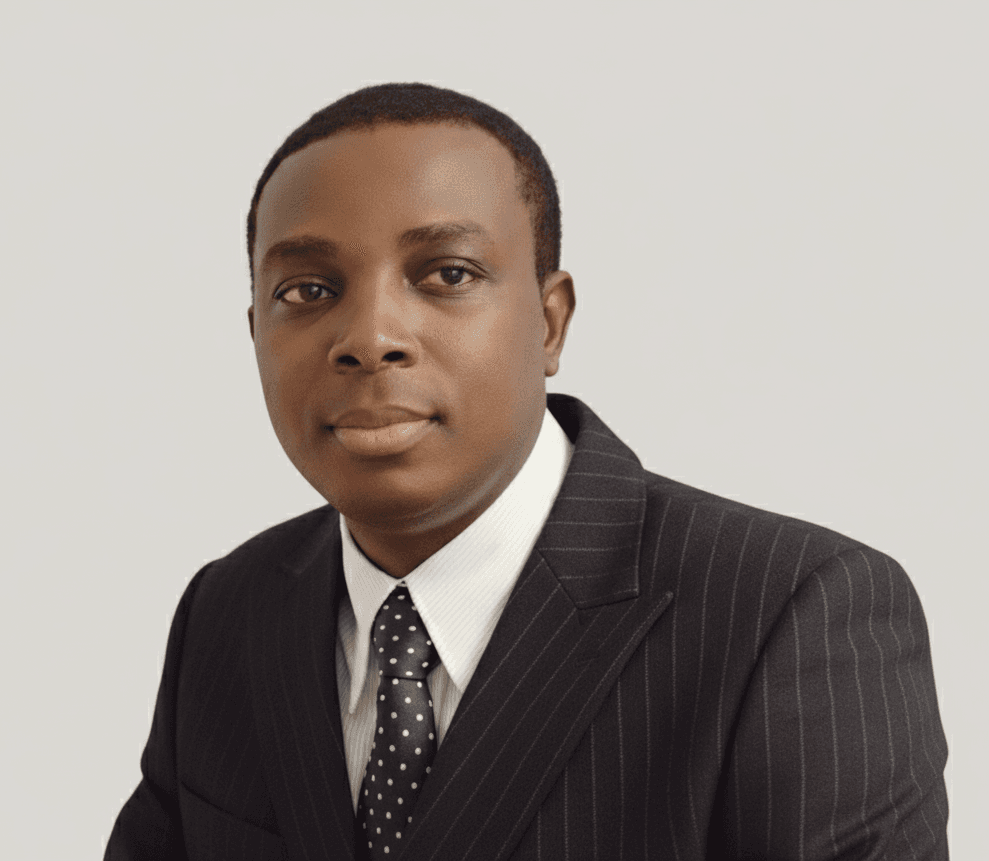
Enyo Ukwela holds an MSc in Aquaculture and Professional Certificates in Project Management and Data Analytics. He is the founder of JILOW Agro (a division of JILOW Horizon Ventures Limited), an integrated agro-industrial enterprise providing agricultural consultancy, project management, talent, data intelligence, and technology solutions across the African agribusiness sector. He writes about aquaculture, agribusiness strategy, leadership, data analytics, AI automation, and business transformation.