Little’s Law
on the Farm
Analyzing the relationship between inventory-in-process and farm throughput times, the equation that manages your warehouse for you.
There is a quiet crisis happening inside thousands of agricultural processing warehouses across Nigeria and sub-Saharan Africa, one that is rarely discussed in agribusiness strategy conversations but that directly determines whether a rice mill, a cassava processing facility, or a groundnut shelling operation generates profit or quietly bleeds it away. It is not a crisis of poor harvests or bad prices. It is a crisis of inventory accumulation.
Bags of un-hulled rice arrive from the field and stack up in receiving warehouses. They arrive faster than the milling lines can process them. Days pass. Then weeks. The bags sit, and while they sit, they cost money, in storage space, in moisture absorption risk, in tied-up working capital that cannot be deployed elsewhere. Eventually the rice is milled, sold, and the cycle repeats, usually with no one having measured how long each bag actually spent in the system or what that residence time cost the business.
Many farm managers instinctively treat this as a spatial challenge: do we have enough square metres to store our bags? But looking at farm inventory through the lens of spatial capacity ignores the underlying financial reality. Storage is not just a spatial problem, it is a dynamic flow problem. And flow problems require flow mathematics. The tool that makes this visible, and solvable, has existed in industrial operations management for over six decades. It is called Little’s Law.
Section 01
Core Framework: Little’s Law
Little’s Law was formally proved by John D.C. Little in 1961, though the intuition behind it had been observed in queuing systems for decades before. In its original form, the law states a relationship between three properties of any stable system through which units flow.
The power of Little’s Law is not in any single form, it is in the relationships it reveals. In a stable system, these three variables are not independent. Change one, and the others must adjust. If WIP grows while throughput rate stays constant, lead time must increase. The mathematics is not optional.
Little’s Law does not judge your operation. It describes it. The judgment comes when you see the numbers and recognize that the lead time you have been accepting is not the lead time your buyers, your product quality, and your working capital can afford.
Section 02 — Case Study
Un-Hulled Rice Accumulation,
Kebbi State Processing Warehouse
A medium-scale rice processing operation in Kebbi State operates a single-line mill with a rated capacity of 3 tonnes of paddy per hour, running two 8-hour shifts per day, a theoretical maximum of 48 tonnes/day. The mill operates at roughly 80% of rated capacity due to maintenance downtime and shift changeover delays, yielding an actual throughput of approximately 38.4 tonnes/day (768 bags/day). During peak harvest season, daily intake averages 1,100 bags (55 tonnes/day), creating an intake-to-throughput gap of 16.6 tonnes/day.
Baseline Parameters
| Parameter | Value |
|---|---|
| WIP inventory (bags) | 8,400 |
| WIP inventory (tonnes) | 420 tonnes |
| Daily intake | 1,100 bags (55 tonnes) |
| Actual daily throughput | 768 bags (38.4 tonnes) |
| Daily WIP growth | +332 bags/day |
| Calculated lead time (Little’s Law) | 10.9 days |
| Management estimate of lead time | ~7 days |
| Lead time underestimation error | 3.9 days (56% error) |
The Lead Time Prediction Table
The mathematical relationship is linear and unforgiving. As WIP accumulates against a fixed throughput rate, lead time scales proportionally:
| WIP (bags) | Throughput (bags/day) | Lead Time (days) | Operational Status |
|---|---|---|---|
| 3,000 | 768 | 3.9 | Well within manageable range |
| 6,000 | 768 | 7.8 | Approaching quality risk threshold |
| 8,400 | 768 | 10.9 | ← Current baseline state |
| 12,000 | 768 | 15.6 | Quality degradation accelerating |
| 16,000 | 768 | 20.8 | Institutional buyer commitments impossible |
The Hidden Holding Costs
Scenario Modelling
| Scenario | WIP (bags) | Throughput (bags/day) | Lead Time | Daily Holding Cost |
|---|---|---|---|---|
| Baseline — no change | 8,400 (growing) | 768 | 10.9 days (rising) | ₦246,400 |
| 2.5 Shifts (+ 4hr partial shift) | 8,400 (stabilizing) | 960 | 8.75 days | ₦194,600 |
| Full second mill line | 8,400 (declining) | 1,536 | 5.5 days | ₦123,200 |
Scenario 2 — extending to 2.5 shifts by adding a partial third shift of 4 hours, required no capital expenditure, only revised labor scheduling and shift incentive payments estimated at ₦85,000 per day. The modelling showed this would stabilize WIP growth, reduce lead time to 8.75 days, and begin drawing down the WIP overhang as the season progressed. The intervention was implemented in week 4. By week 6, WIP had reduced to 6,100 bags and lead time had contracted to 6.4 days, validating the Little’s Law prediction to within 8% error, and reducing daily holding cost by approximately ₦87,000.
Section 03
Little’s Law as a
Continuous Management Tool
The Daily Five-Minute Dashboard
From these three numbers, a manager can calculate current WIP, current lead time, and whether the system is accumulating or drawing down its inventory overhang. This takes five minutes per day and requires no software. The discipline is not technical. It is managerial: the commitment to measure these three numbers every single day and act when the trend line points the wrong direction.
Back-Calculating the Required Throughput Rate
This calculation converts what is often a vague aspiration, “we want faster turnaround”, into a precise engineering target. The conversation stops being “we feel we need a second milling line” and becomes “to honor our institutional buyer commitment of 5-day turnaround at peak-season WIP levels, we require 2,400 bags/day throughput, here is the gap, and here is what closes it.”
Throughput Improvement — Sequenced by Capital Intensity
Section 04 — Critical Thinking
The Four Consequences of Swelling
Inventory Against Fixed Processing Speed
If WIP increases while throughput rate remains constant, Little’s Law is unambiguous: lead time must increase proportionally. There is no mathematical escape from this relationship. But the practical implications extend well beyond the arithmetic, when lead time extends, a cascade of second-order effects begins.
Conclusion
The Equation That
Manages Your Warehouse
There is something satisfying about a mathematical law that requires no software, no advanced training, and no expensive implementation to apply. Little’s Law, WIP equals throughput rate times lead time, can be written on a whiteboard in a Nigerian rice mill office, populated with numbers from a physical count and a processing log, and used to generate more operationally actionable insight in 20 minutes than most warehouse management systems produce in a month of reporting.
The Kebbi State operation did not need a consultant to tell them their lead time was 10.9 days. They needed a framework that connected the three numbers they already had, bags in stock, bags processed per day, and time, and revealed what those numbers meant together. Little’s Law was that framework.
Applied consistently, as a daily check, a weekly trend review, a scenario-planning tool for harvest season capacity decisions, Little’s Law transforms a warehouse from a passive accumulation space into a managed flow system with visible, measurable, and controllable performance parameters. For agricultural processing operations working under seasonal pressure, thin margins, and intensifying institutional buyer requirements, this transformation is not academic. It is operational survival.
Count the bags. Know the rate. Calculate the lead time.
Manage the consequence before it manages you.
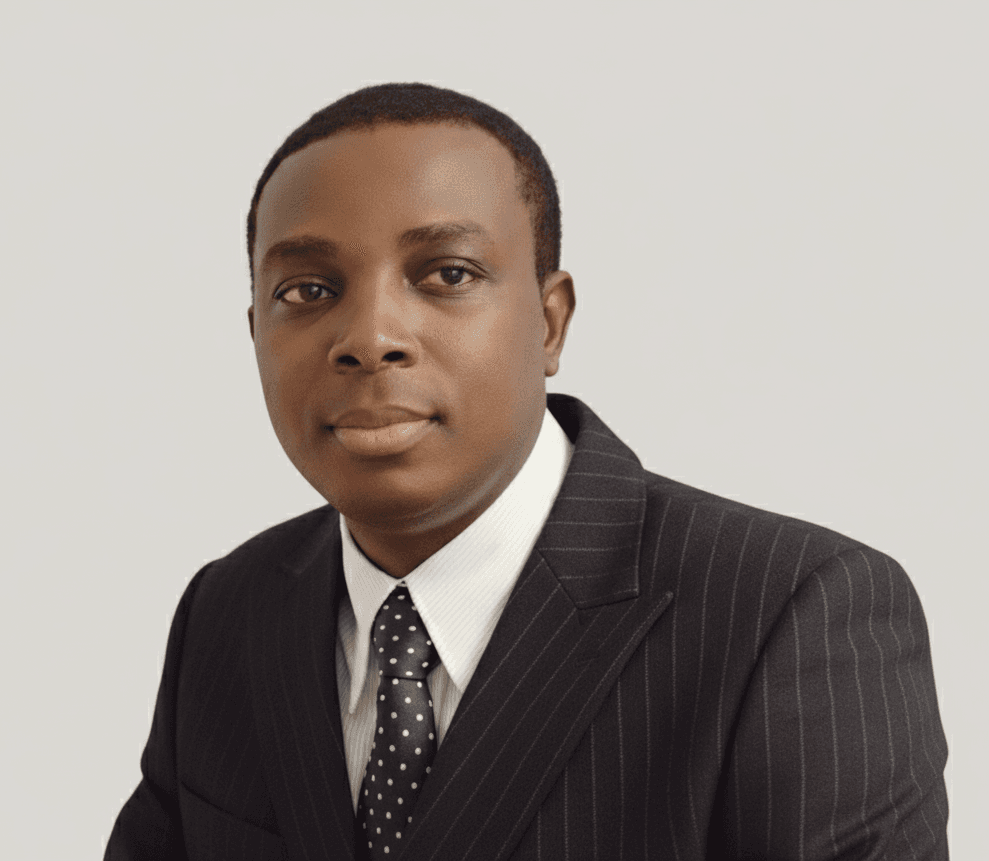
Enyo Ukwela holds an MSc in Aquaculture and Professional Certificates in Project Management and Data Analytics. He is the founder of JILOW Agro (a division of JILOW Horizon Ventures Limited), an integrated agro-industrial enterprise providing agricultural consultancy, project management, talent, data intelligence, and technology solutions across the African agribusiness sector. He writes about aquaculture, agribusiness strategy, leadership, data analytics, AI automation, and business transformation.